
Squeeze Casting Explained: Direct, Indirect and Local Squeeze Compared with HPDC
High-pressure die casting fills a die in milliseconds and accepts some trapped air as the price of speed. Squeeze casting reverses the priorities: the metal enters slowly and calmly, and the pressure stays on until the casting has solidified. The result is a dense, low-gas part – at the cost of cycle time.
What Is Squeeze Casting?
Squeeze casting is a permanent-mould process in which molten metal fills a preheated steel die with little turbulence and then solidifies under high pressure. Total Materia describes it as “liquid-metal forging”; the pressure is held until the casting is completely solid, which suppresses gas and shrinkage porosity.
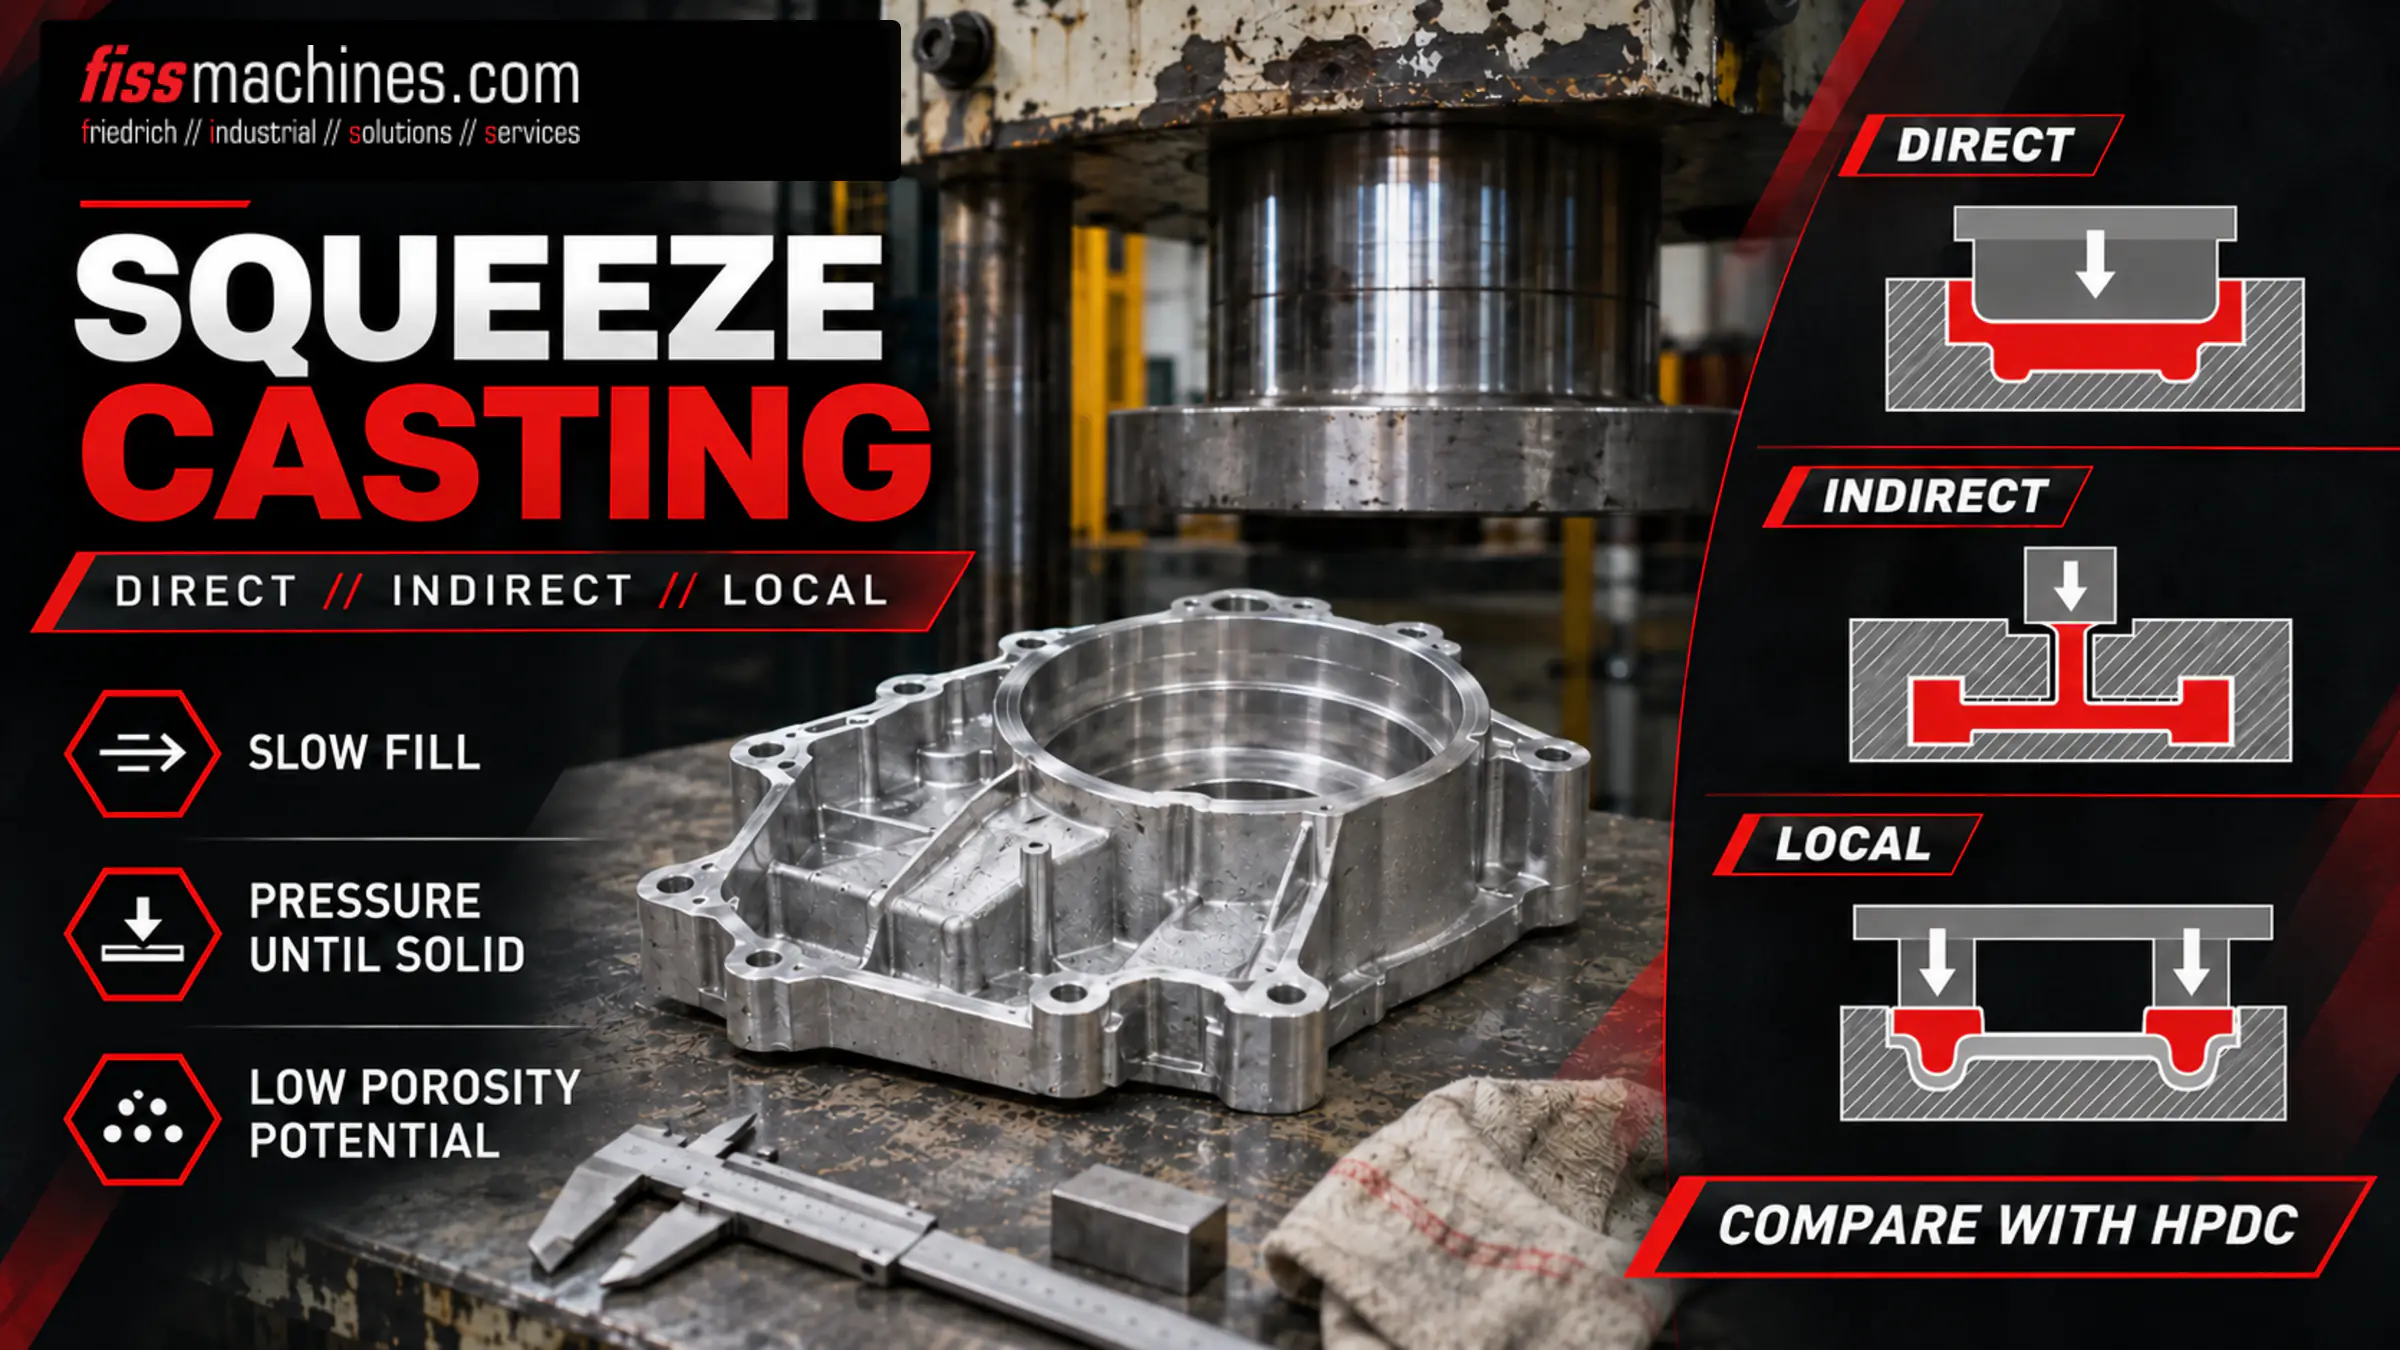
In direct squeeze casting a punch presses on the metal, in indirect squeeze casting a plunger fills the closed die through wide gates. Local squeeze applies the idea to single hot spots in an HPDC die.
How Does Squeeze Casting Work?
Squeeze casting separates filling and pressurising: slow filling lets air escape ahead of the melt front, pressure then acts on metal that is still feeding. Total Materia names die temperatures of 190–315 °C and pressures of 50–140 MPa as normal values, the Open University 30–110 MPa “depending on component geometry and material”. These are literature values, not settings.
Prepare the Die
The die is preheated and coated with release agent; die temperature controls how fast the skin forms.
Fill Slowly
Metal enters with little turbulence. A 2013 Indian Foundry Congress paper gives about 0.3–0.35 m/s gate velocity for alloy 356 as typical, against roughly 20–45 m/s in conventional HPDC.
Pressurise
The punch or plunger builds up pressure shortly after filling and holds it until the casting is solid, feeding shrinkage as it occurs.
Open and Eject
The die opens, the part is ejected and, where required, heat treated and machined.
Because squeeze casting works with liquid metal, it is not a semi-solid process. Semi-solid routes such as thixocasting and rheocasting start from a partly solid slurry; they are compared in Thixomolding Explained.
Direct or Indirect Squeeze Casting: Where Does the Pressure Act?
A Papervision patent (US 5,908,065) summarises the two squeeze casting variants and their weaknesses. The difference lies in where the pressure enters the casting.
Punch on the Casting
Metal is ladled into the lower die; the upper die closes and presses on most of the casting surface. No runners or feeders, high metal yield, usually in a vertical hydraulic press. Pouring is turbulent and dosing sets part weight.
Plunger Through the Gate
A plunger fills the closed die through wide gates and holds pressure via the gating system. Closer to die casting and more productive, but porosity can remain far from the plunger and runners add circulating metal.
According to the same patent, direct squeeze casting can also process alloys with poor fluidity, while indirect squeeze casting suits conventional casting alloys. In indirect squeeze casting, runners and biscuit can exceed half of the shot mass – metal that goes back to the furnace.
Vertical Squeeze Casting Machines
Industrial indirect squeeze casting mostly runs on machines with a vertical shot unit, so the melt rises from below and air is pushed upwards. UBE Machinery offers two series (manufacturer statement, product page archived April 2025): VSC with vertical die clamping and vertical shot, 200–800 t clamping force, and HVSC with horizontal toggle clamping and vertical shot, 350–1,200 t.
- Inclined docking: the sleeve is filled in a tilted position, swings upright and docks into the die; UBE states this keeps the melt warm and enables “ultra-low-speed shot”.
- Two-stage clamping (VSC): locking force switches from low to high during injection to help degassing.
- Pitless shot unit available as an option for the HVSC (manufacturer statement).
On a used squeeze casting machine, check above all the docking and tilting mechanism, sleeve and plunger, and how stably the control holds very low shot speeds and the hold pressure.
Local Squeeze: Squeeze Pins in HPDC Dies
Many die castings have a few thick bosses that solidify last and cannot be fed once the gate has frozen. A local squeeze pin targets exactly these spots. A Toshiba Machine patent (US 5,787,963) describes pressing the pin into the melt “immediately before” it solidifies, driven by its own squeeze pin cylinder.
Fracchia et al. (TMS 2022) studied local squeeze for thick sections of complex aluminium automotive parts where design changes were not possible and intensification or cooling could not remove shrinkage porosity, with leak tightness as the target. Where hot spots sit is best predicted by simulation – see Casting Simulation in Die Casting.
Squeeze Casting vs Die Casting, Low-Pressure and Gravity Casting
The table places squeeze casting among the permanent-mould processes (qualitative comparison).
| Criterion | Squeeze Casting | HPDC | Low-Pressure | Gravity |
|---|---|---|---|---|
| Filling | Slow, low turbulence | Very fast, turbulent | Slow, from below via riser tube | Poured, often with tilting |
| Pressure during solidification | High, held until solid | Intensification after filling | Low gas pressure | Metallostatic only |
| Air entrapment during filling | Low (slow fill) | Higher, unless vacuum is used | Low (calm fill) | Depends on pouring |
| Solution heat treatment | Possible | Only with low-gas process | Common | Generally possible |
| Wall thickness | Medium to thick | Thin walls possible | Medium to thick | Typically thicker |
| Cycle time | Long | Very short | Longer than HPDC | Longer than HPDC |
Details of the two neighbouring processes are covered in Low-Pressure Die Casting Explained and Gravity Die Casting or High-Pressure Die Casting?
Typical Squeeze Casting Applications and Heat Treatment
Squeeze casting is chosen for safety-relevant, compact aluminium parts that need high strength, ductility or pressure tightness. The Open University names wheels, hubs and pistons; an SAE paper (1999) by Delphi and Casting Technology Company describes converting cast-iron front knuckles to squeeze-cast aluminium. UBE states that its squeeze castings can be welded because they contain less gas than conventional die castings (manufacturer statement).
Low gas content is also the key to heat treatment. The 2013 congress paper gives gas contents as low as 1 cm³ per 100 g aluminium and concludes that T6 and welding are possible. Why conventional die castings blister in solution treatment is explained in Heat Treatment of Aluminium Die Castings. The Open University advises wider tolerances to allow for distortion during heat treatment.
Limits of Squeeze Casting and When It Pays Off
Squeeze casting is not a general replacement for HPDC. The Open University cites 5–30 shots per hour and calls process control demanding. The 2013 paper reports longer cycles and a coarser microstructure than HPDC; Total Materia points to macrosegregation. Thin, large-area parts remain the domain of HPDC with vacuum.
- The part is compact or thick-walled and safety-relevant
- Solution heat treatment (T6) or welding is required
- Porosity or leak-tightness limits are strict
- Volumes justify a dedicated machine, but not the cost of forging
- If only a few hot spots cause scrap: test local squeeze in the existing HPDC die first
Porosity types and their causes are explained in Die Casting Defects Explained.
Squeeze Casting Trades Speed for Integrity
Squeeze casting combines slow, calm filling with high pressure during solidification and produces dense, heat-treatable and weldable aluminium parts. Indirect squeeze casting on vertical machines brings the process closer to series production. Where only a few spots of a die casting are porous, local squeeze pins are often the cheaper first step – provided timing and pin position are found by trial.
Questions About Squeeze Casting
Is Squeeze Casting the Same as Semi-Solid Casting?
No. Squeeze casting fills the die with fully liquid metal and then solidifies it under pressure. Semi-solid processes such as thixocasting or rheocasting inject a partly solid slurry. Both aim at low porosity, but feedstock and equipment differ.
What Is the Difference Between Direct and Indirect Squeeze Casting?
In direct squeeze casting a punch presses straight onto the metal in the die, without runners. In indirect squeeze casting a plunger fills the closed die through gates and holds pressure via the gating system. Indirect is closer to die casting and more productive; direct offers higher metal yield.
Can a Conventional HPDC Machine Do Squeeze Casting?
Not in the full sense: squeeze casting needs very low, controlled shot speeds, wide gates and a long hold-pressure phase, as provided by dedicated machines with vertical shot units. A standard HPDC machine can run local squeeze pins if hydraulics and control support the extra cylinders.
Are Squeeze Castings Heat Treatable?
Generally yes, because their gas content is low. Sources describe T6 heat treatment and welding as possible. The alloy must be heat-treatable, and distortion during quenching should be considered in tolerances.
Used Die Casting Machines from FISS.
FISS lists used die casting machines and searches the market for specific equipment on request. Tell us which process and clamping force you need.
Sources
Total Materia: Squeeze Casting Process: Part One, June 2007, totalmateria.com, accessed 19 November 2026.
The Open University (OpenLearn): Squeeze casting and squeeze forming, open.edu, accessed 19 November 2026.
M. Thirugnanam: Modern High Pressure Die-casting Processes for Aluminium Castings, Transactions of the 61st Indian Foundry Congress, 2013.
Papervision Ltd: Apparatus and method for squeeze casting, US Patent 5,908,065, 1999.
Toshiba Machine Co.: Squeeze pin control system in die casting machine, US Patent 5,787,963, 1998; Q. Han: Method for reducing local defects in a casting, US Patent 11,597,008 B2, 2023.
E. Fracchia, F. S. Gobber, C. Mus, R. Pirovano, M. Rosso: The Local Squeeze Technology for Challenging Aluminium HPDC Automotive Components, TMS 2022 Annual Meeting, abstract.
D. T. Gerken, R. Neal: Squeeze Cast (SCPM) Light Weight Aluminum Front Knuckle Case Study, SAE Technical Paper 1999-01-0344, abstract.
UBE Machinery Corporation: HVSC Series / VSC Series – Squeeze Casting Machines, product page (archived 24 April 2025), accessed 19 November 2026.